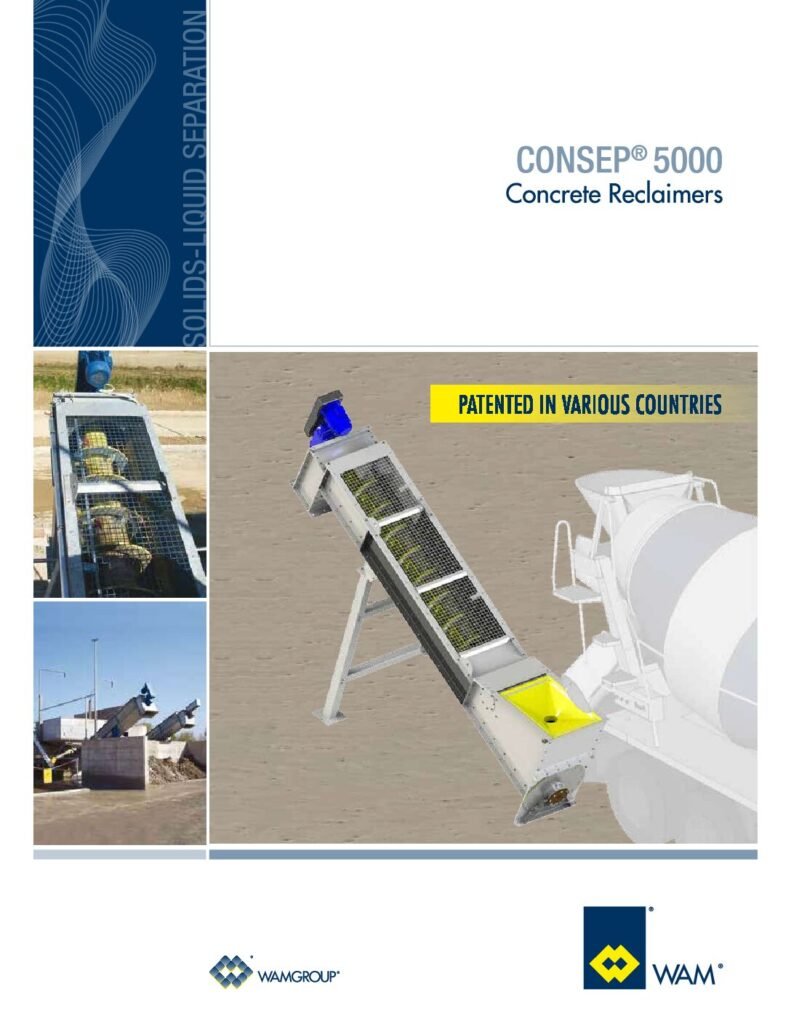
WAM® Concrete Recycling Systems provide efficient solutions for the recovery and recycling of residual concrete and wash water generated at ready-mixed concrete and precast concrete plants.
The systems separate aggregates from cement-rich wash water, allowing valuable materials to be recovered and wastewater to be managed more efficiently.
The CONSEP® range is designed for the treatment of returned concrete from truck mixers and concrete pumps, helping concrete producers reduce waste, improve resource utilisation and comply with environmental requirements.
Depending on the required capacity and plant configuration, CONSEP® systems can be supplied as individual reclaimers or as complete systems with dedicated feeding arrangements for multiple truck mixers.
CONSEP® 5000
Maximum capacity: up to 20 m³/h of returning concrete
Separation of aggregates into two particle-size categories
Aggregate classification at approximately 5 mm
High-efficiency solids-liquid separation
Configurations with or without dedicated screw feeder
Available in S, L and T configurations
T configuration allows simultaneous discharge of multiple truck mixers
Main Advantages
Recovery of valuable aggregates from returned concrete
Recycling of concrete wash water
Reduction of concrete waste
Reduced environmental impact
Reduced consumption of fresh water
Improved housekeeping around the concrete plant
Efficient aggregate washing
High-efficiency solids-liquid separation
Low running and maintenance costs
Wear-resistant components
Compact and robust design
Flexible configuration for different plant capacities
Suitable for integration into existing concrete plants
Typical Applications
Ready-mixed concrete batching plants
Precast concrete plants
Concrete truck-mixer washing areas
Concrete pump washing stations
Recovery of residual concrete
Recycling of concrete wash water
Aggregate recovery
Cement-rich slurry water management
Concrete production facilities
Plants looking to reduce concrete waste and water consumption